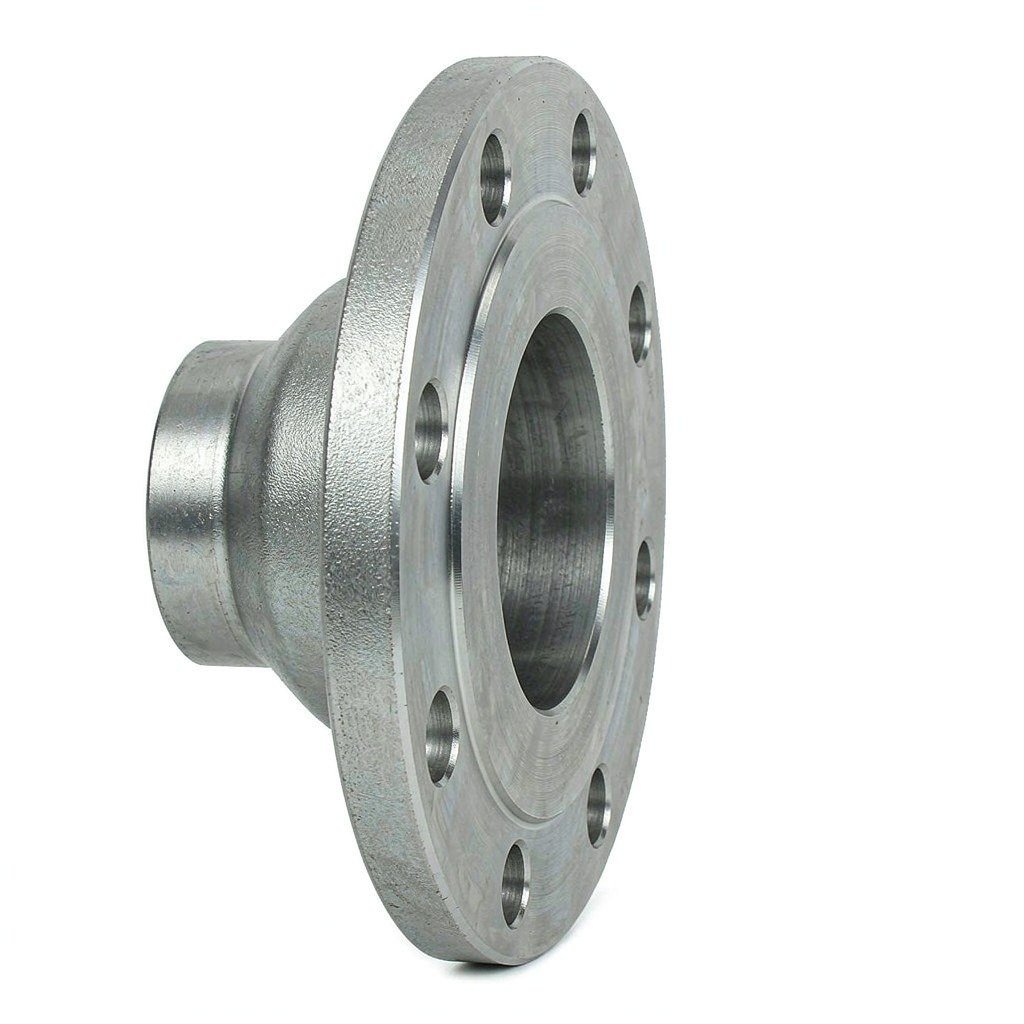
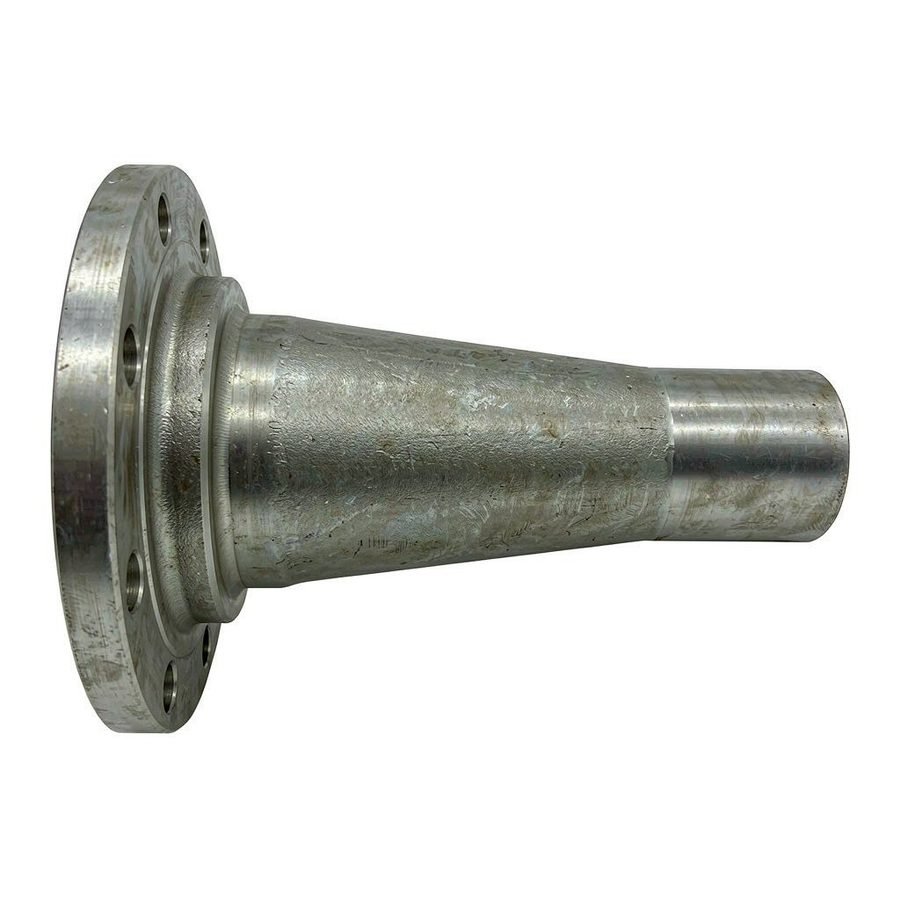
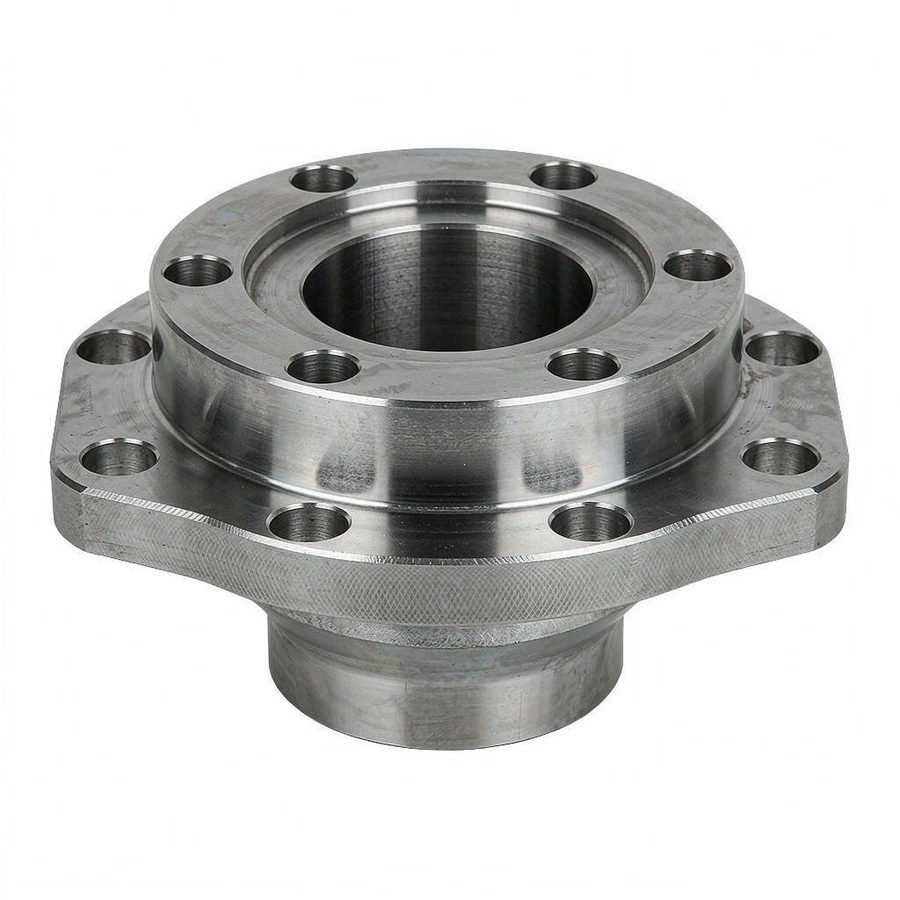
A weld-neck flange has a tapered hub and a bevelled end for a full-penetration circumferential weld rather than a fillet weld. The hub transfers load from the pipe into the flange body smoothly, which is why this type goes on lines with pressure and thermal cycling. Hub thickness and bore follow the pipe schedule and the bevel angle follows the drawing. For PN up to 40 we work to the GOST 12821-80 tables, for PN up to 250 to GOST 33259-2015 (type 11).
The sealing face is type B (raised face) by default, with types A, C, D and E to drawing; the face must match the mating flange or the joint will not hold. For critical service the lot can ship with non-destructive testing — ultrasonic or radiographic examination of the weld to an agreed procedure. The heat number is marked on every item and lot documents are ready before shipment.